What we are known for
Stainless Steel Fabrication
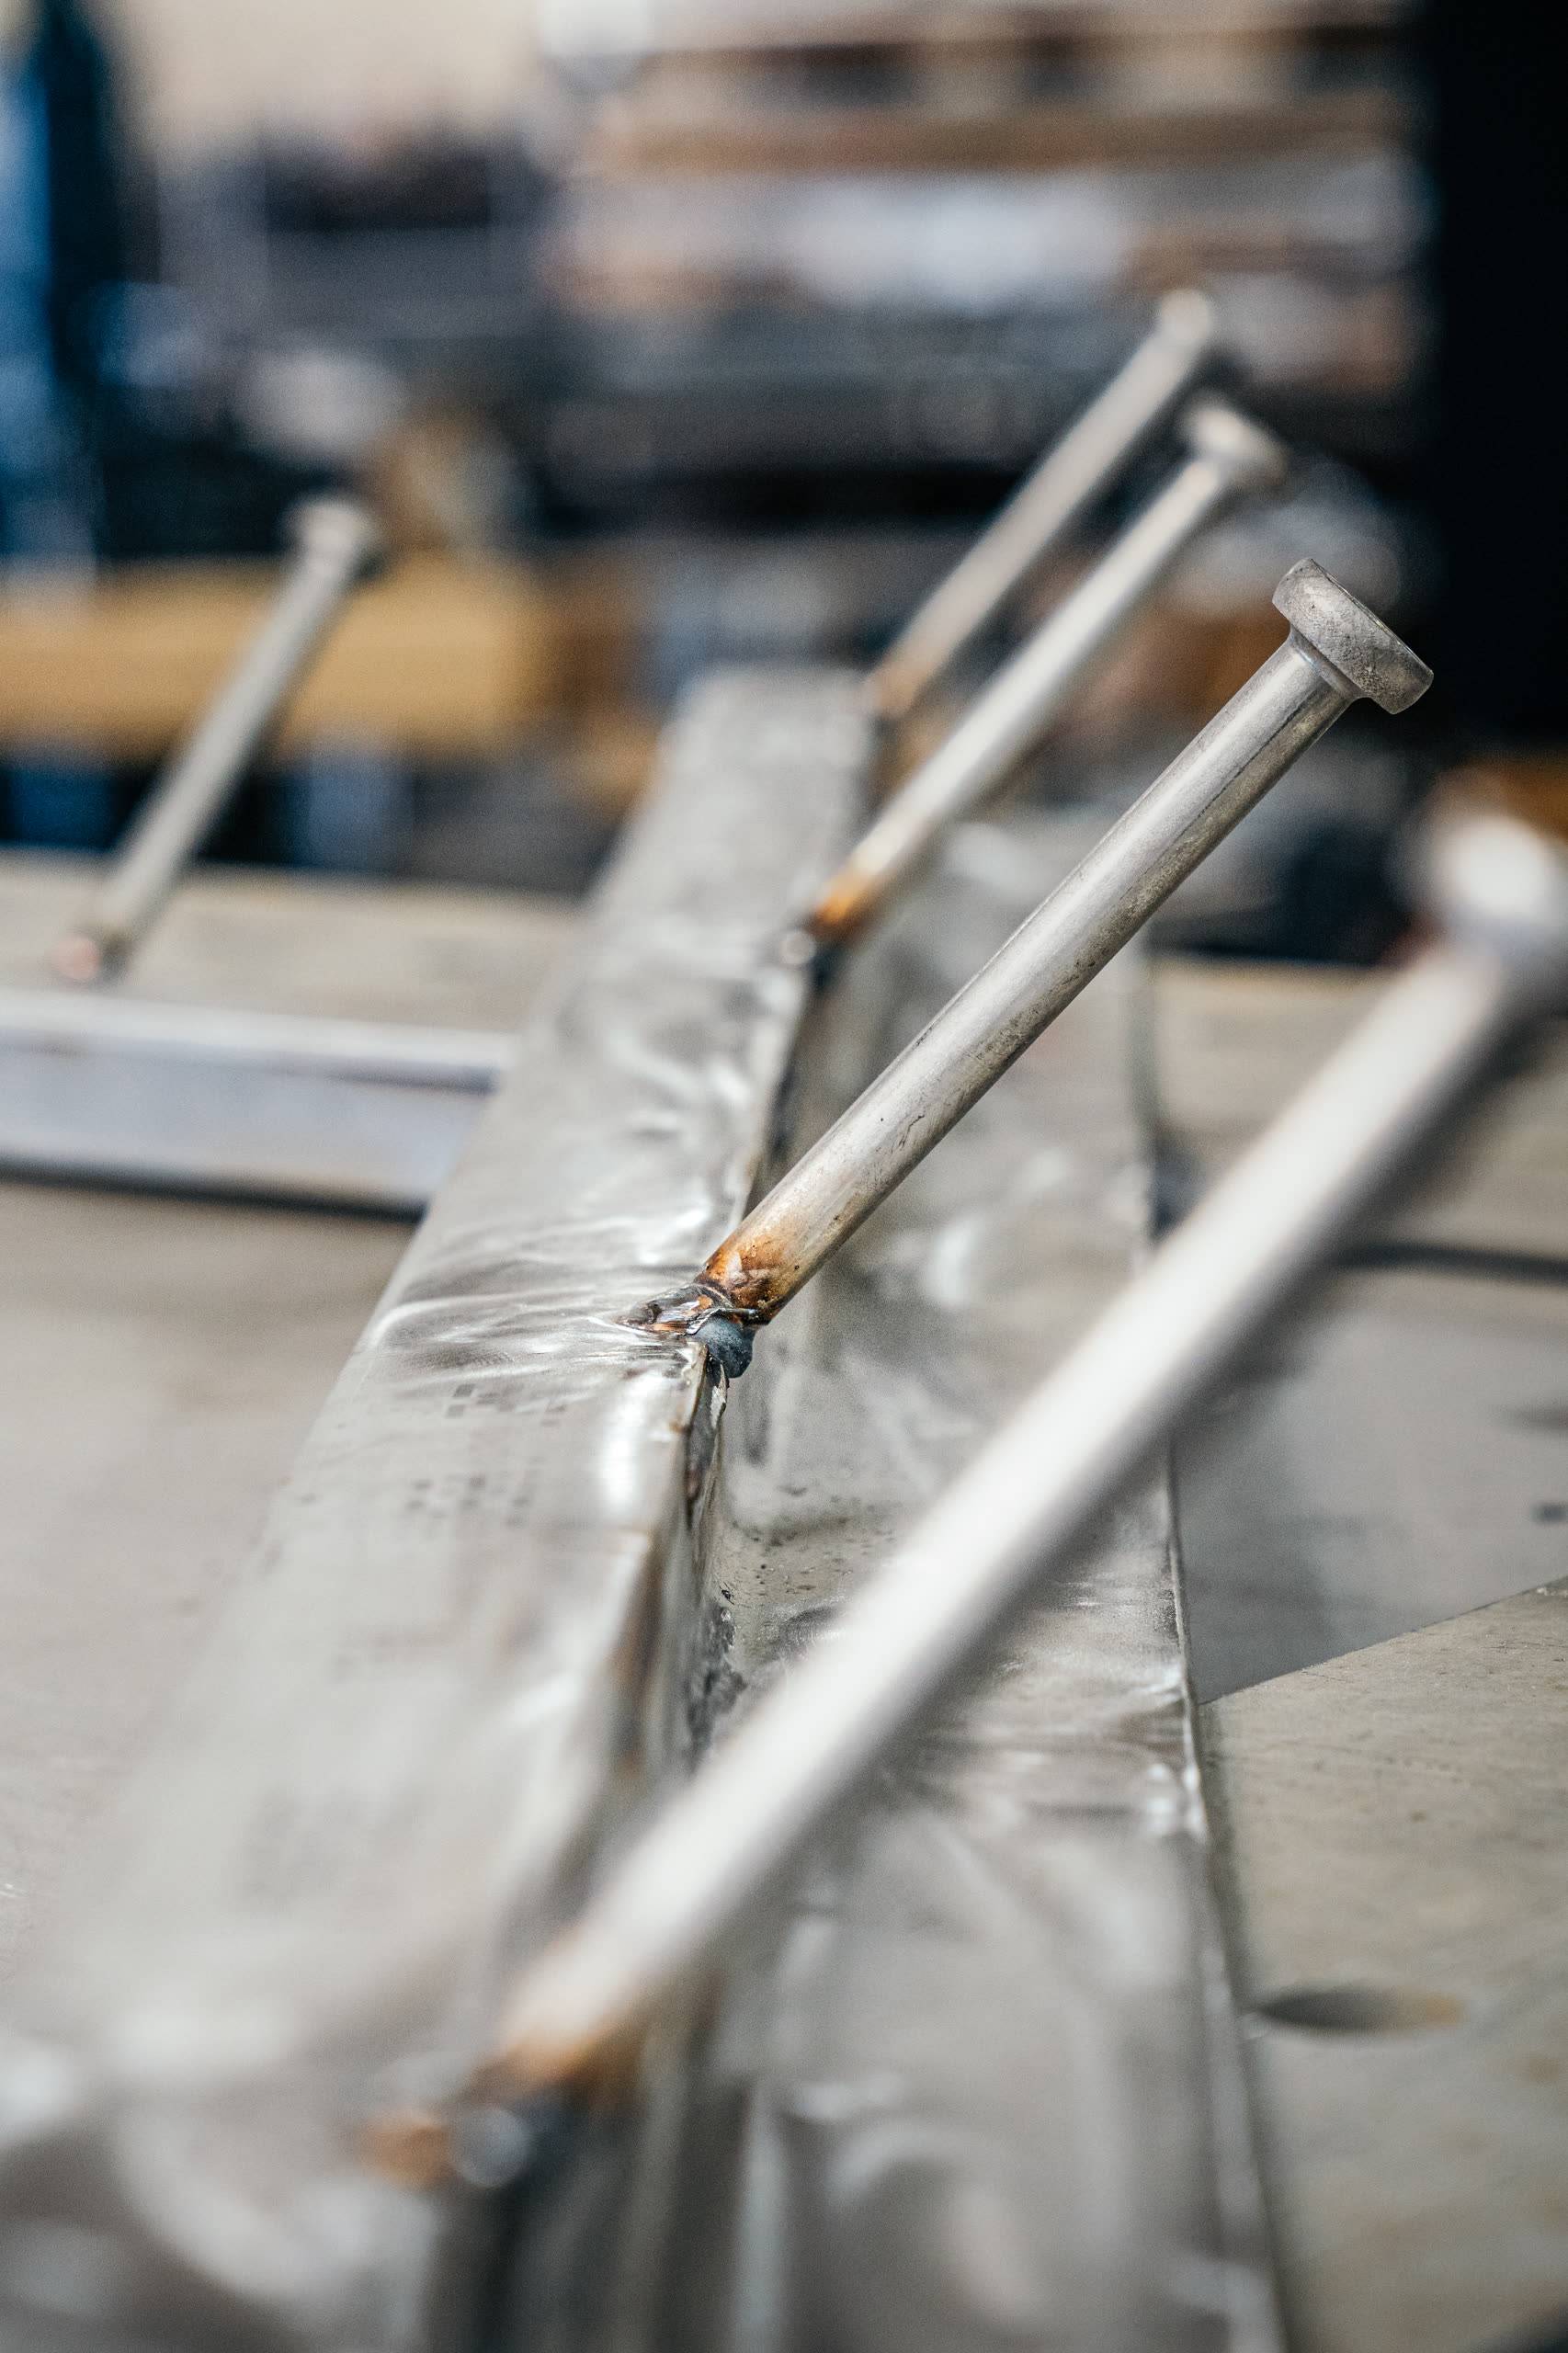
South Coast Iron fabricates stainless steel in volume from Placentia, California. We laser cut stainless up to 1.5 inches thick on a 20 kW sheet laser, weld it, and polish it in house rather than sending it out. Most of our competitors are structural steel shops that occasionally touch stainless. We are the other way around.
- Metal Fabrication
- Structural Steel
- Custom Fabrication
- Access & Safety Systems
- Silos & Hoppers
- Laser Cutting
At a glance
Specifications
| Sheet thickness | Up to 1.5 in on the 20 kW laser |
|---|---|
| Sheet size | 74 in x 168 in, dual shuttle tables |
| Tube and section | 0.75 in to 14 in square, 6 kW tube laser with bevel head |
| Tolerance | Approximately plus or minus 0.0010 in on tube |
| Finishing | Polishing in house, satin through mirror |
| Turnaround | Same day, or one to two days |
What we cover
- Sheet stainless cut up to 1.5 in thick
- Tube, pipe and section from 0.75 in up to 14 in square
- In house polishing to satin, brushed or mirror
- Same day or one to two day turnaround on cut parts
Why stainless separates shops
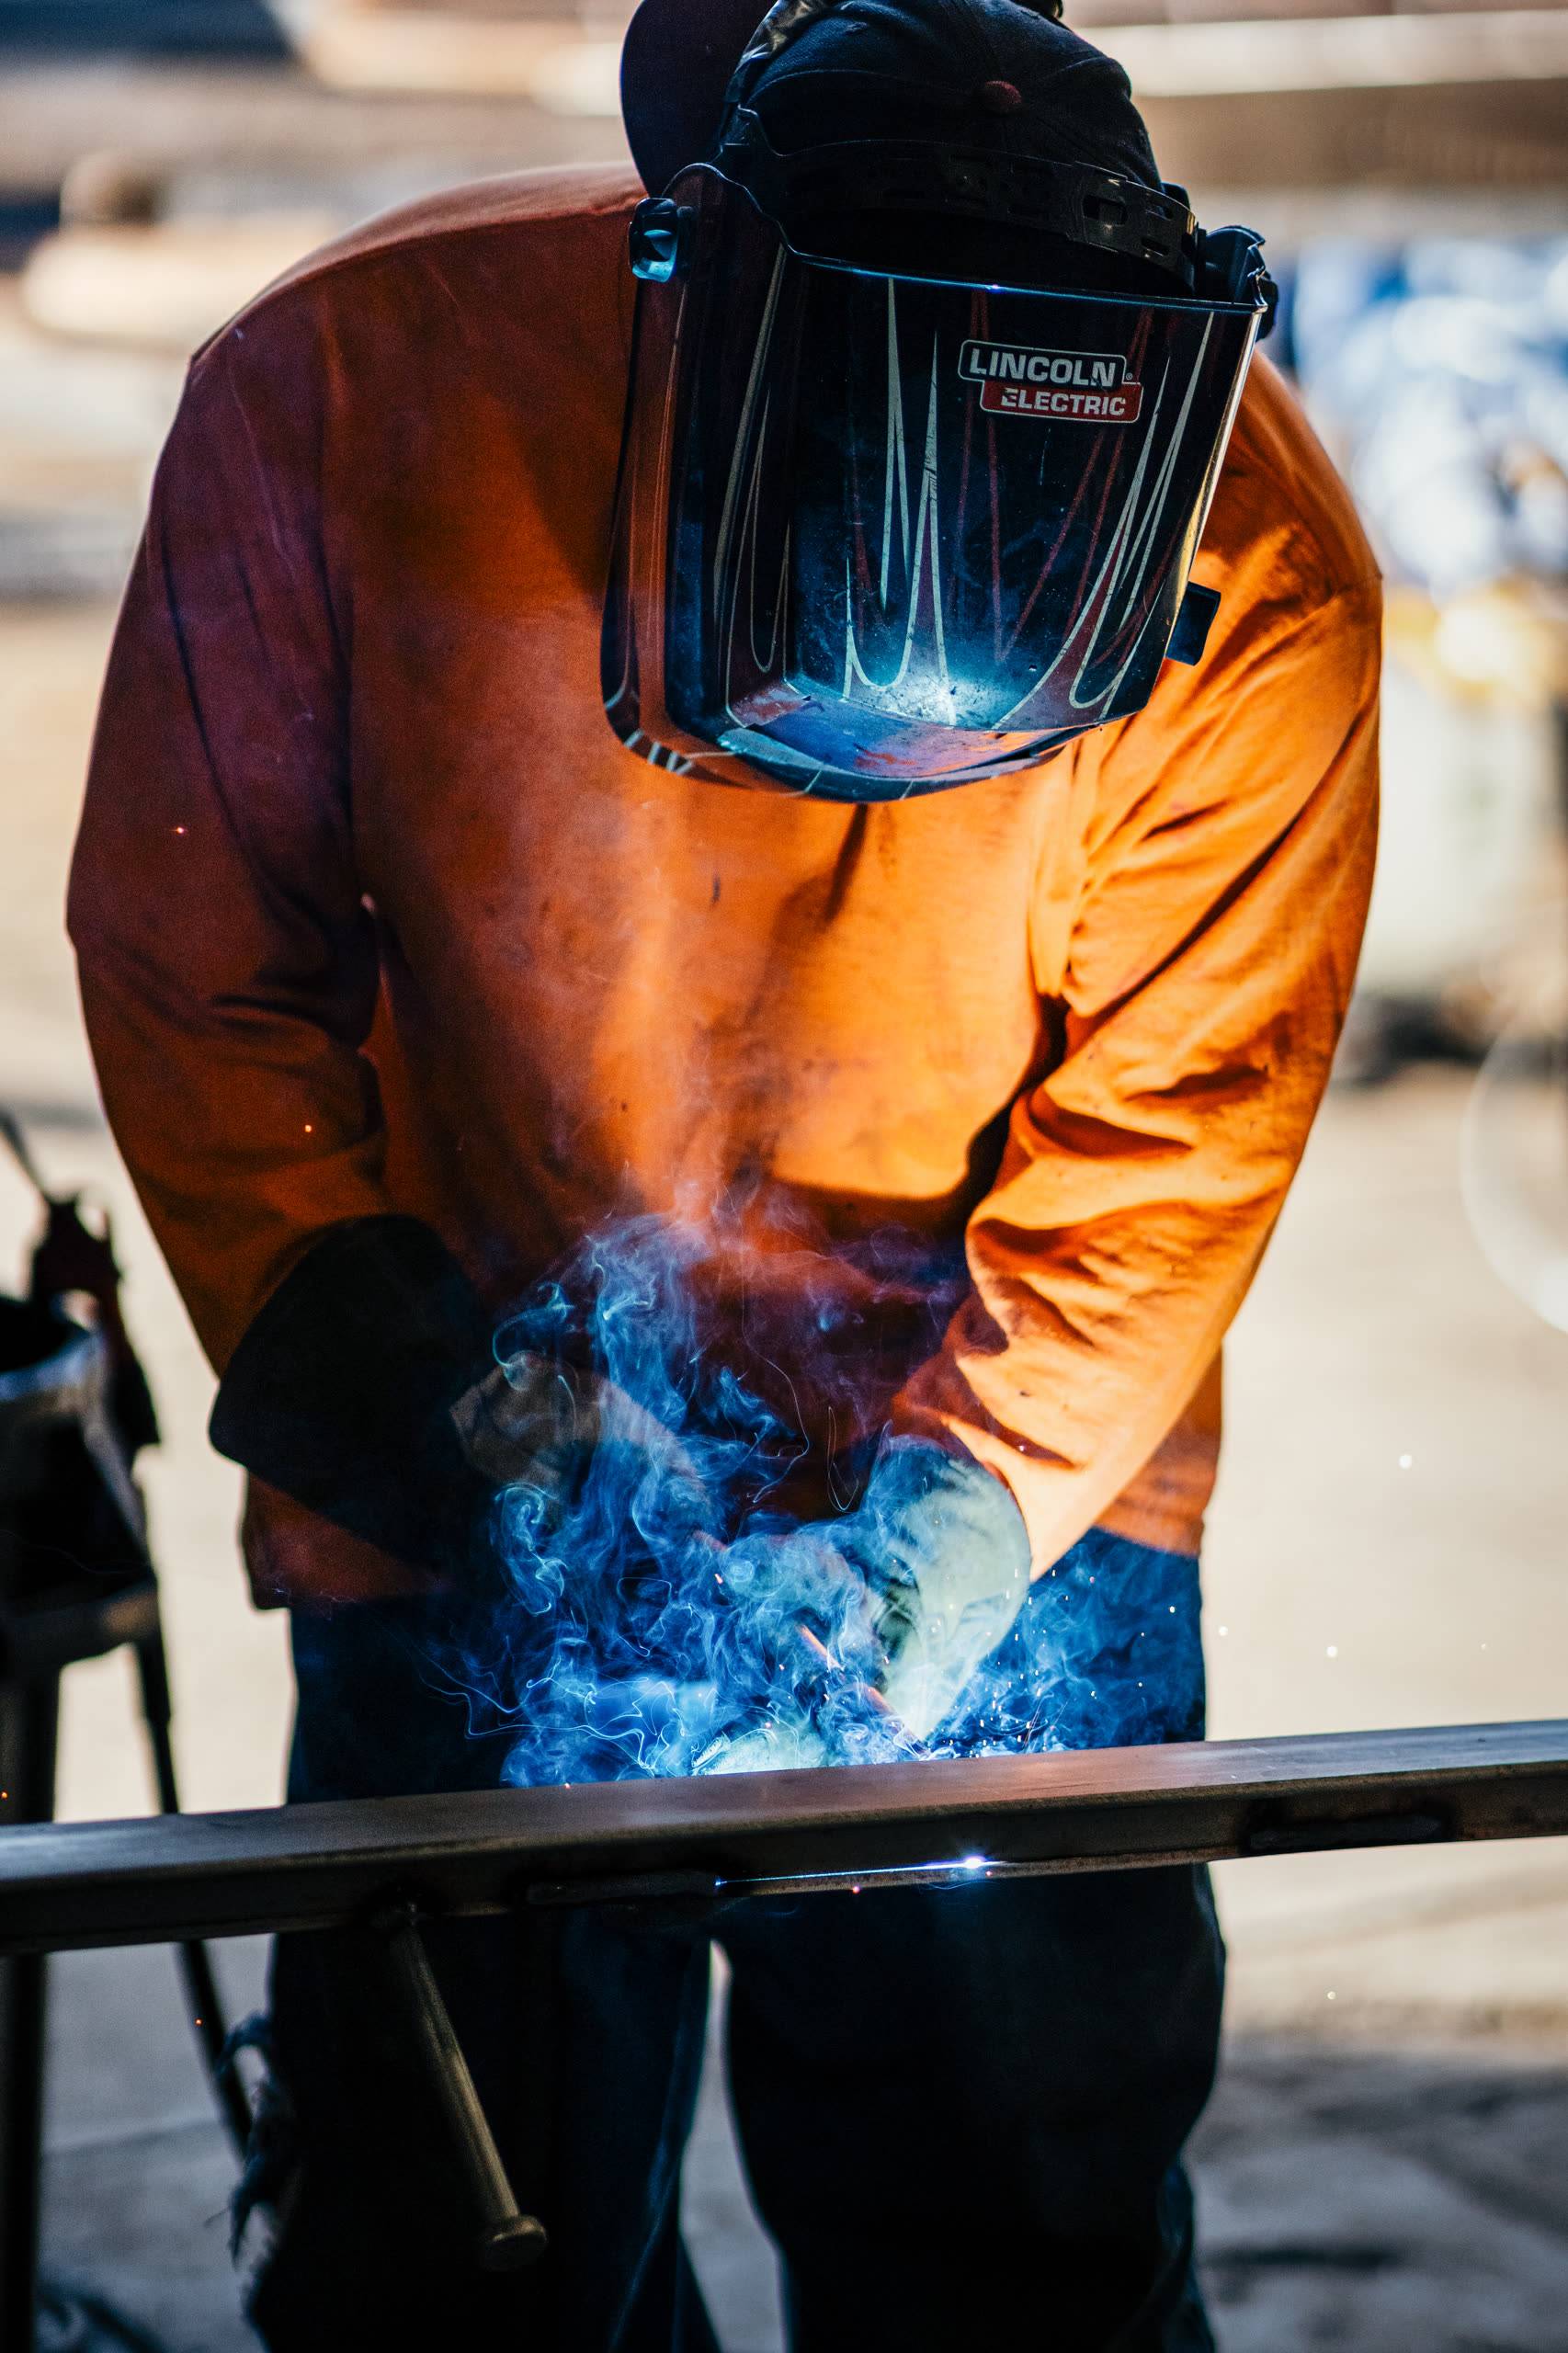
Stainless behaves differently from carbon steel at every stage. It moves more under heat, so a weld sequence that works on mild steel will pull an assembly out of square. It work hardens, so a drill that wanders once will not get a second chance. And the finish is part of the product rather than something applied afterwards, which means every weld has to be dressed and blended rather than ground flat and painted over.
None of that is difficult if you do it every week. It is very difficult if you do it twice a year. That is the whole difference, and it is why a shop can quote stainless confidently and still deliver something that has to be reworked on site.
Cut first, then weld less
Most of the cost in a stainless assembly is not the material. It is the labor in fitting and finishing. The way we take that cost out is by cutting the parts accurately enough that they locate themselves.
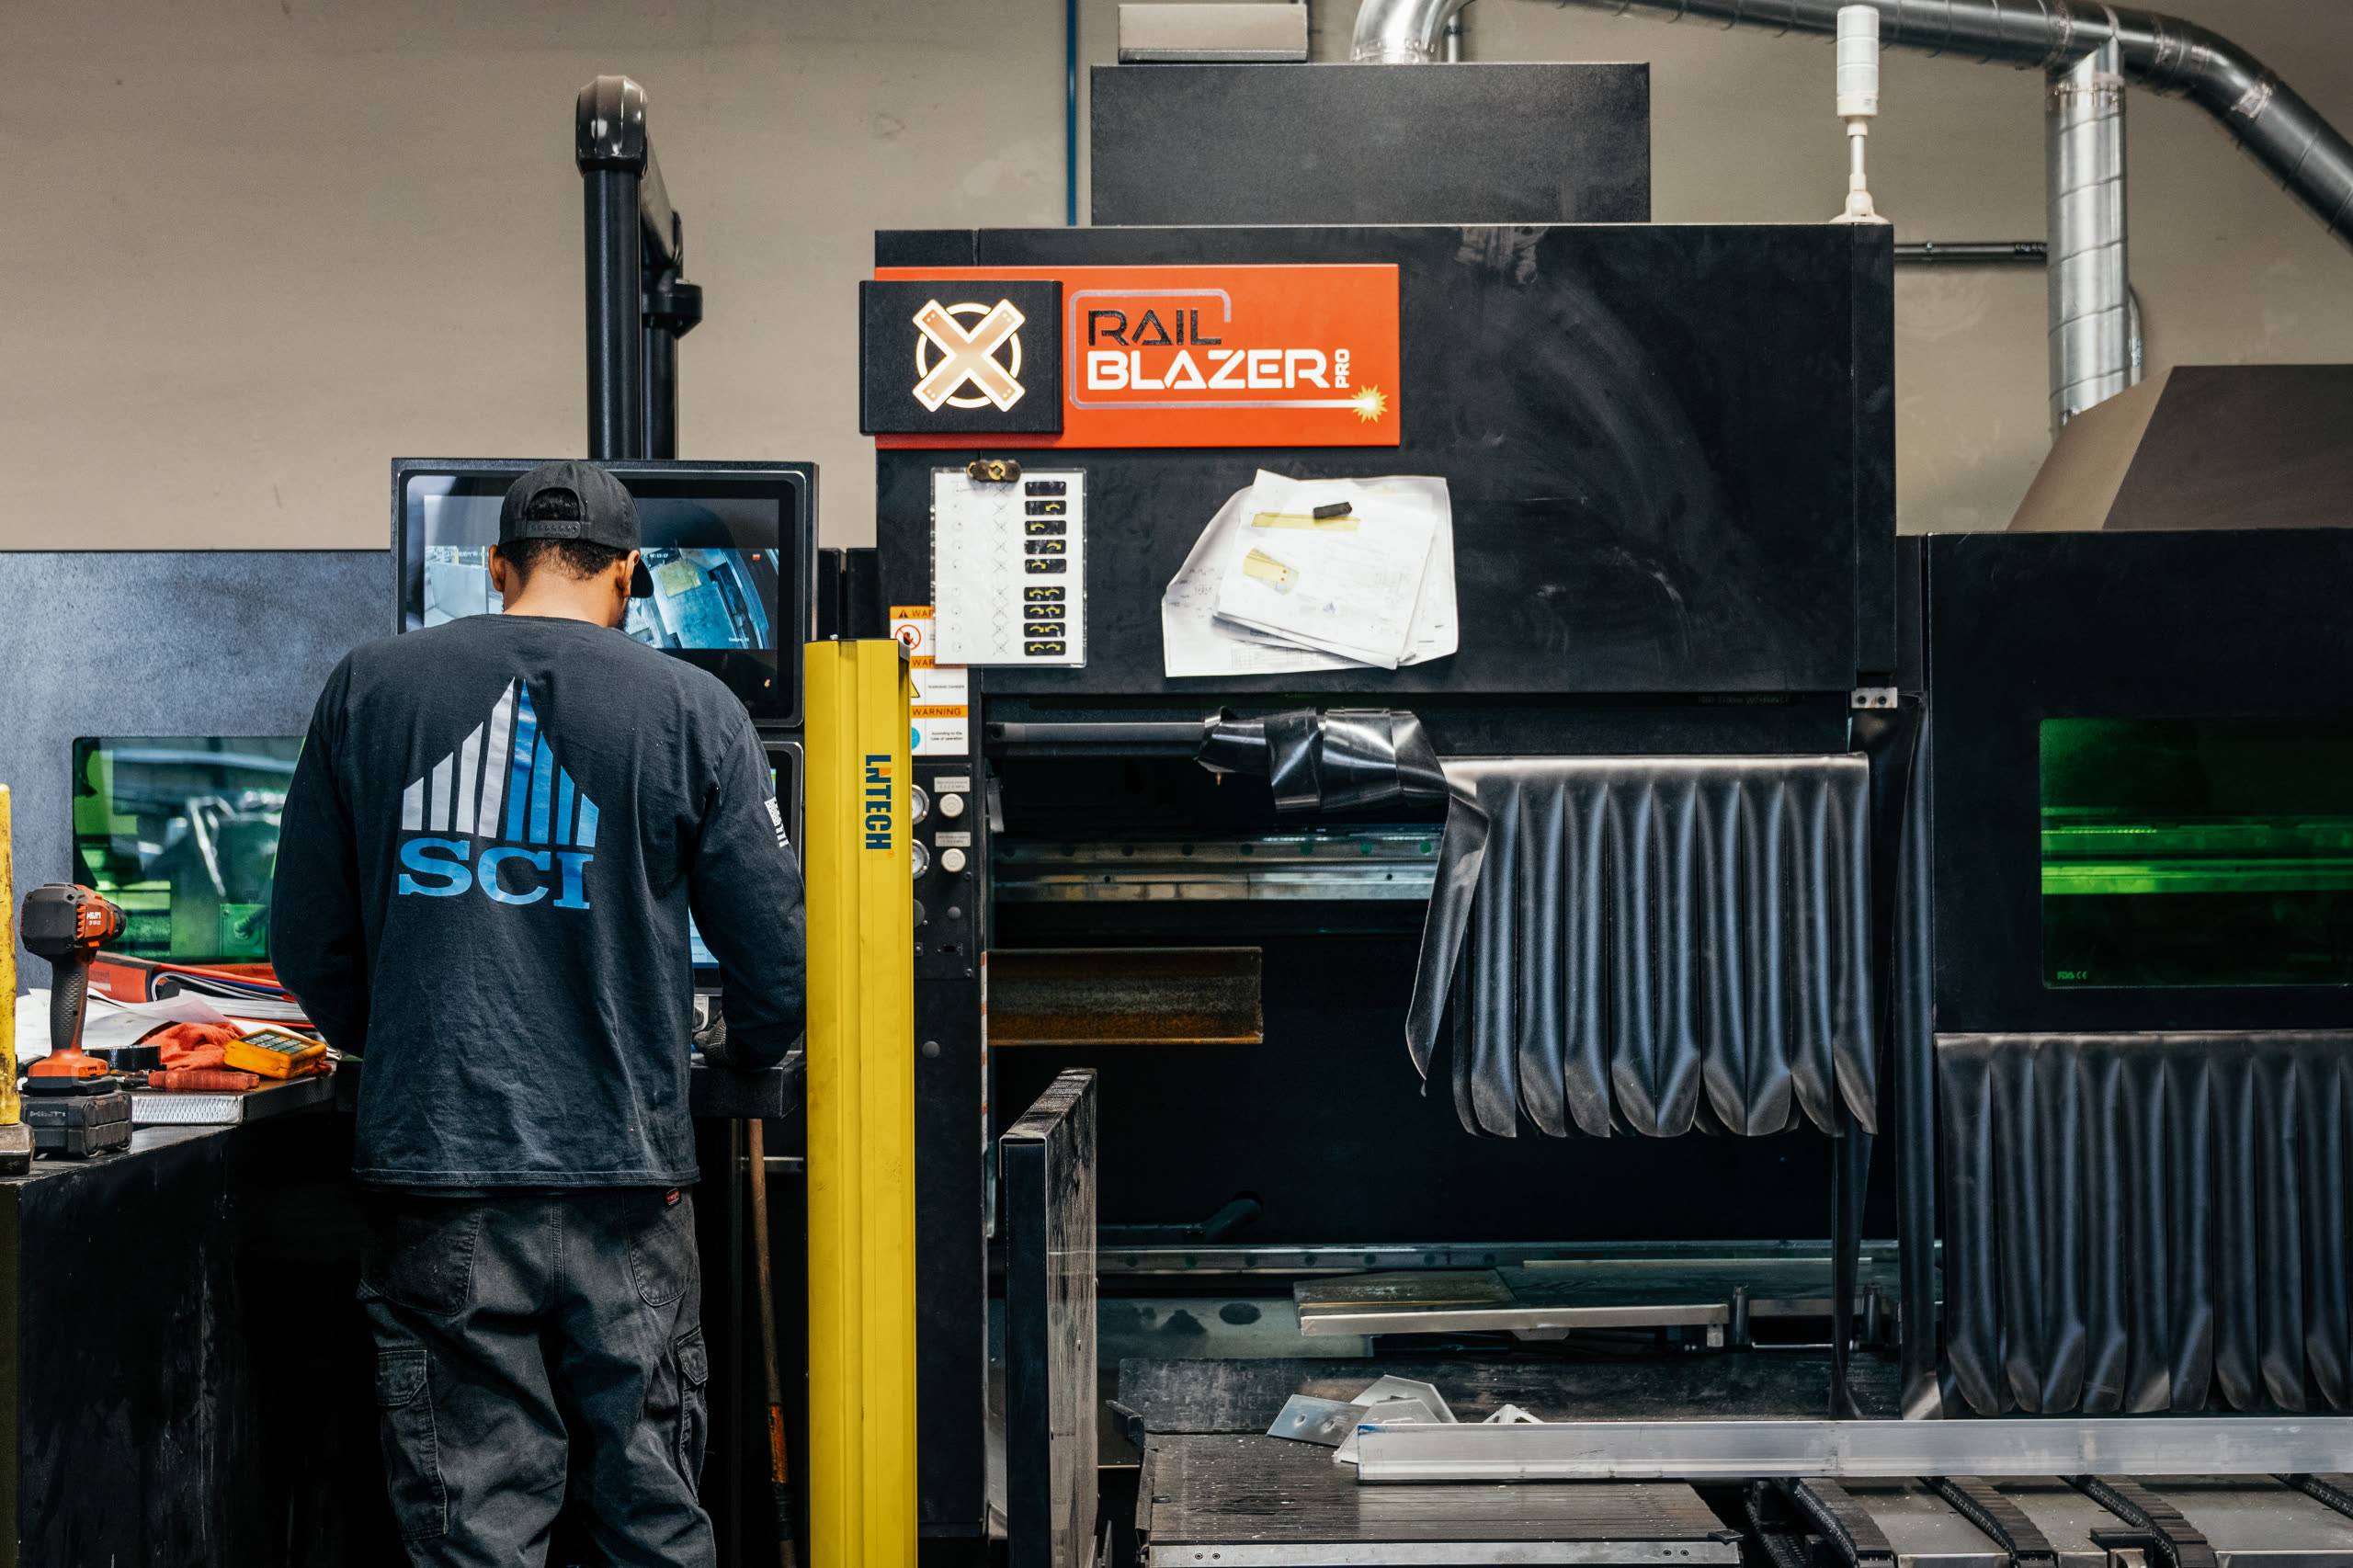
Our tube laser cuts copes, holes, slots and weld prep straight into the section, so a railing post arrives with its rail notch already cut rather than being ground to fit at the bench. On sheet work the 20 kW laser cuts bend lines and bolt patterns in the same pass. Less fitting means fewer welds, fewer welds mean less distortion, and less distortion is what keeps a polished finish looking right.
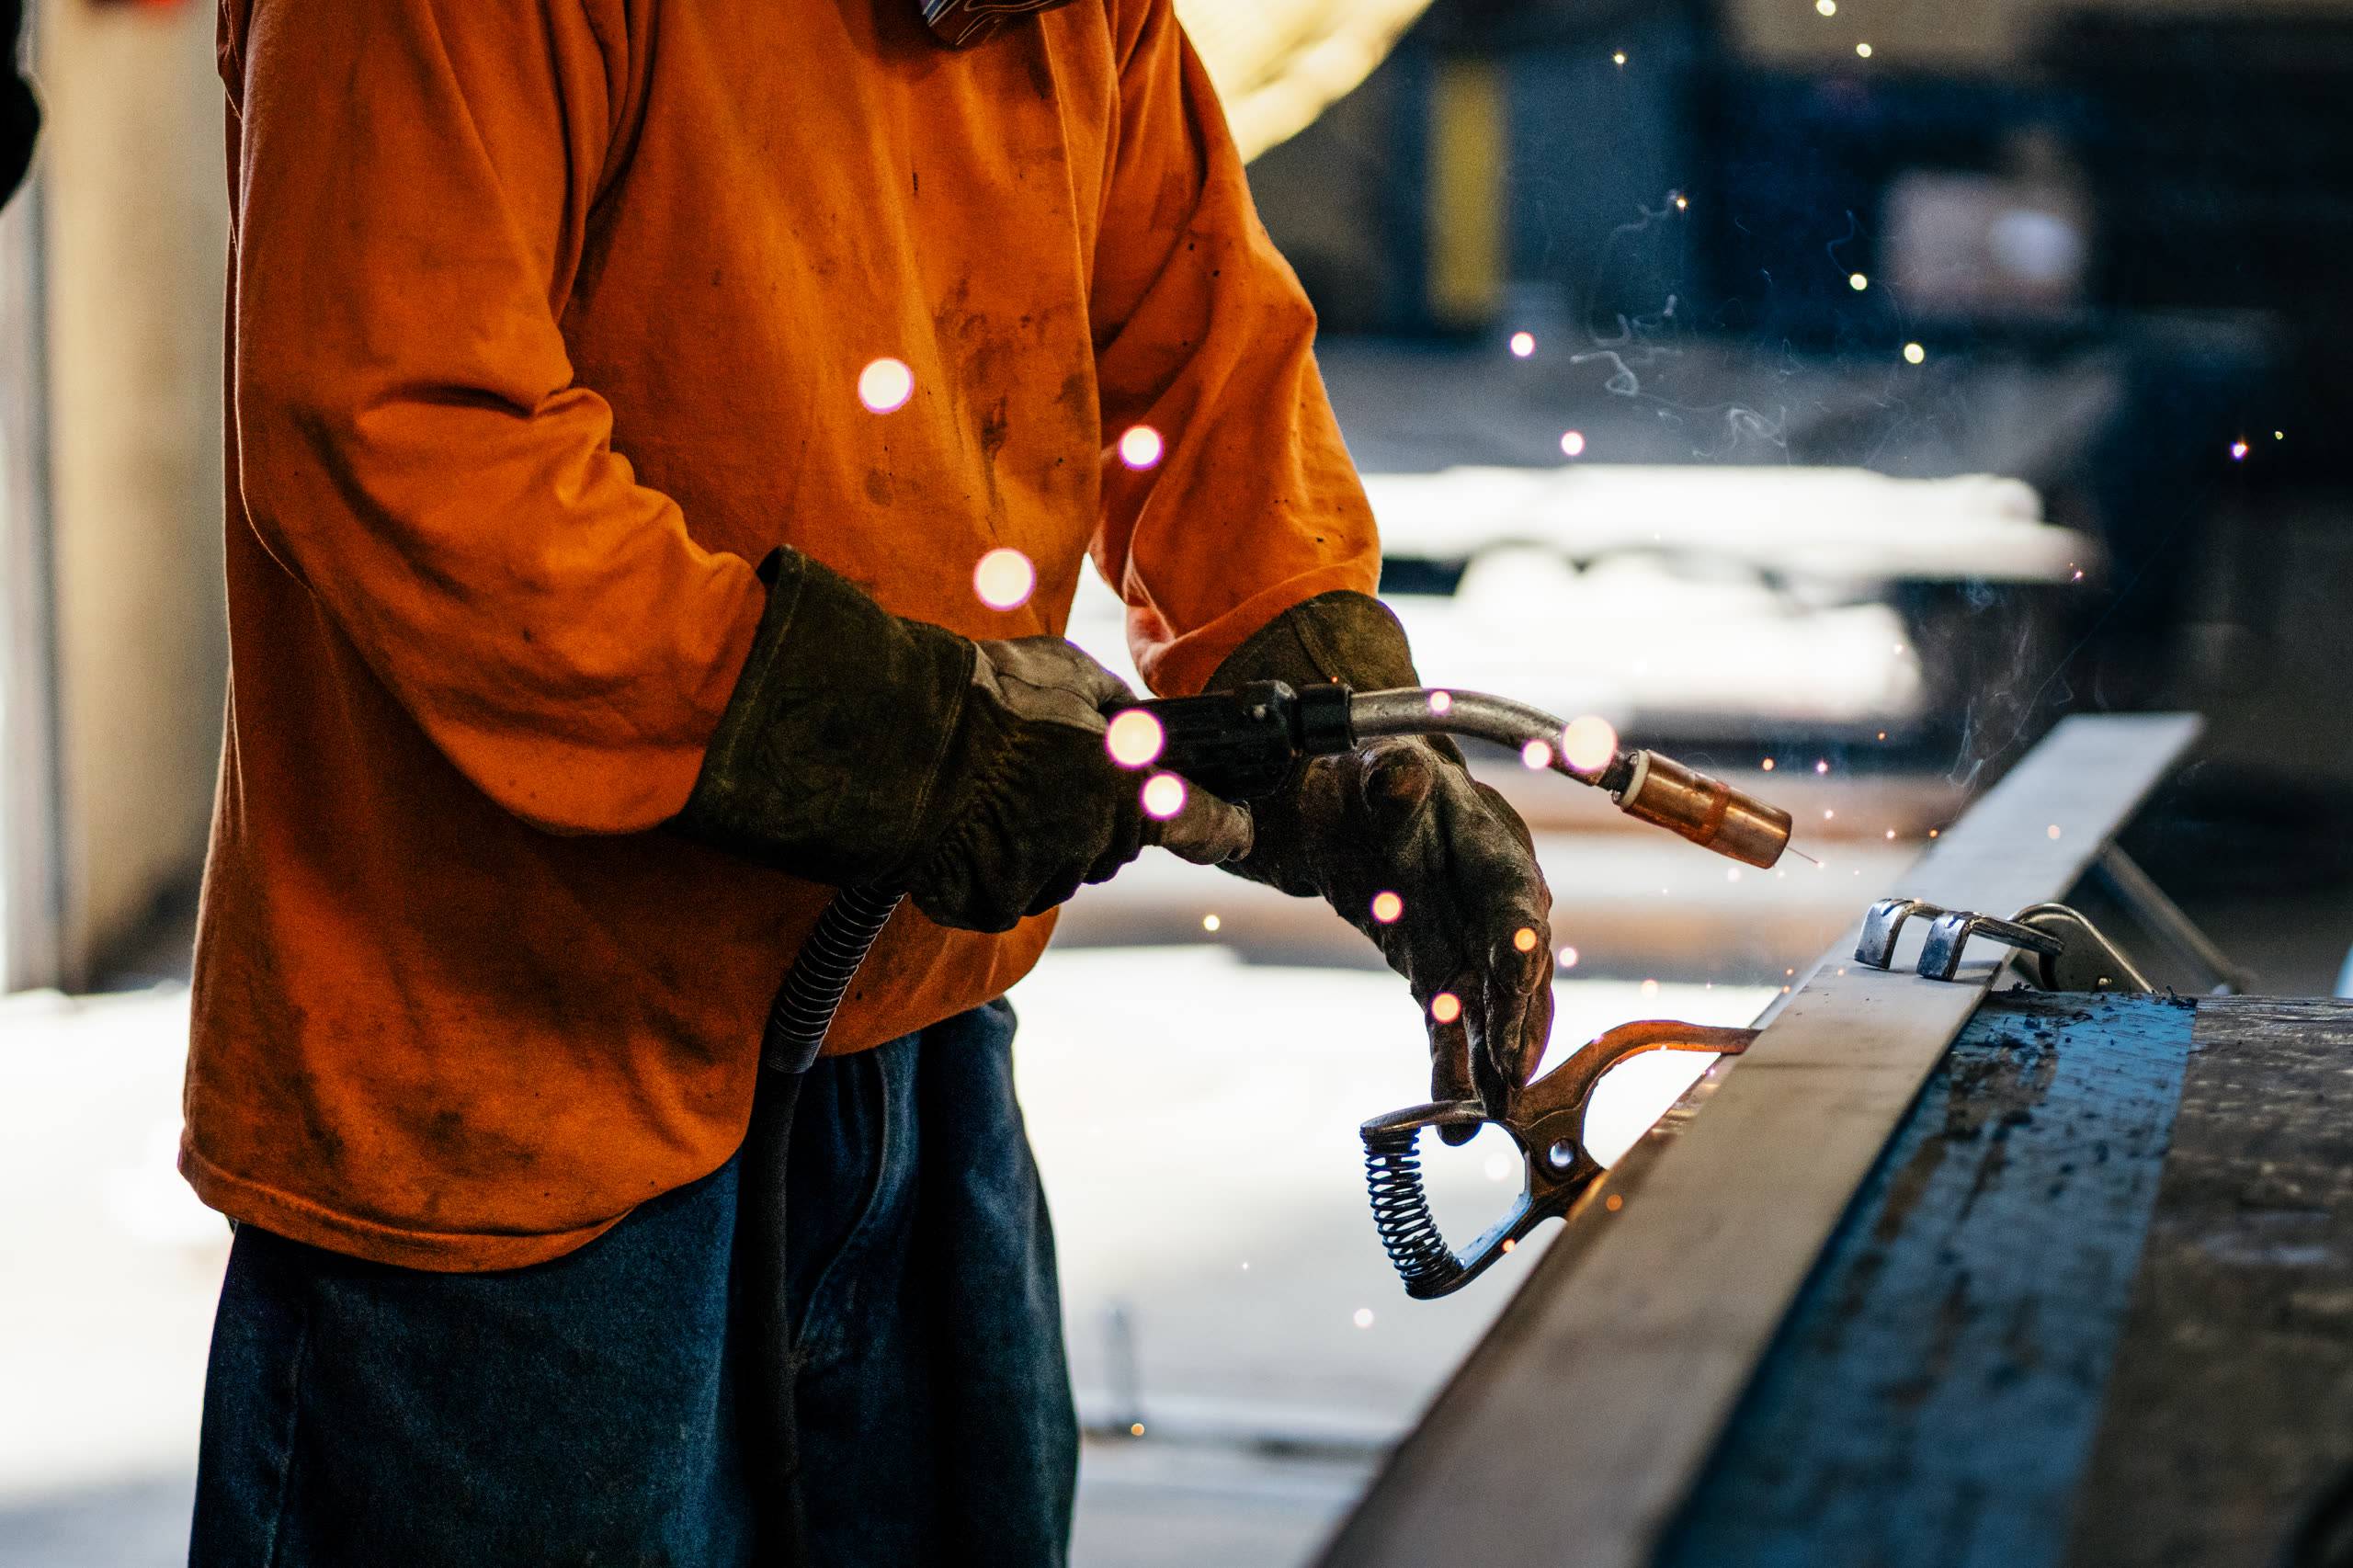
Where our stainless work ends up
Railings and handrail are the biggest single category, from simple cable rail through to polished theme park handrail where every reflection is inspected. Water treatment is the next, where stainless silos, hoppers and platforms have to survive chemistry that would eat coated carbon steel.
Beyond that it is architectural work, which is where the polishing matters most, and food and beverage equipment work where the finish is a hygiene requirement rather than an aesthetic one.
Before you call
Questions we get asked
Not answered here? The fastest route is a phone call to the shop.
Got a drawing? Talk to the shop.
Call and we will talk it through, or send the scope and drawing set and we will get back to you with pricing and a schedule.