Cut in, not ground on
Tube Bevel and Weld Prep
South Coast Iron cuts weld bevels, copes and fit up features directly into tube and structural sections using a bevel head on our 6 kW tube laser. The prep arrives as part of the member rather than being ground in by hand at the bench.
- Metal Fabrication
- Structural Steel
- Custom Fabrication
- Access & Safety Systems
- Silos & Hoppers
- Laser Cutting
At a glance
Specifications
| Bevel | Bevel head on the 6 kW tube laser |
|---|---|
| Features | Bevels, copes, saddles, slots, tabs, locating holes |
| Sections | Tube, pipe, channel, W beams, angle, WTs |
| Size range | 0.75 in round to 14 in x 14 in square |
| Tolerance | Approximately plus or minus 0.0010 in |
| Detailing | In house, SolidWorks |
What we cover
- Weld bevels cut to the angle the procedure calls for
- Copes and saddles matched to the mating member
- Slots, tabs and locating features for self fixturing assemblies
- Square, rectangular and round tube, pipe, channel, beams and angle
Hand prep is the hidden cost in a welded assembly
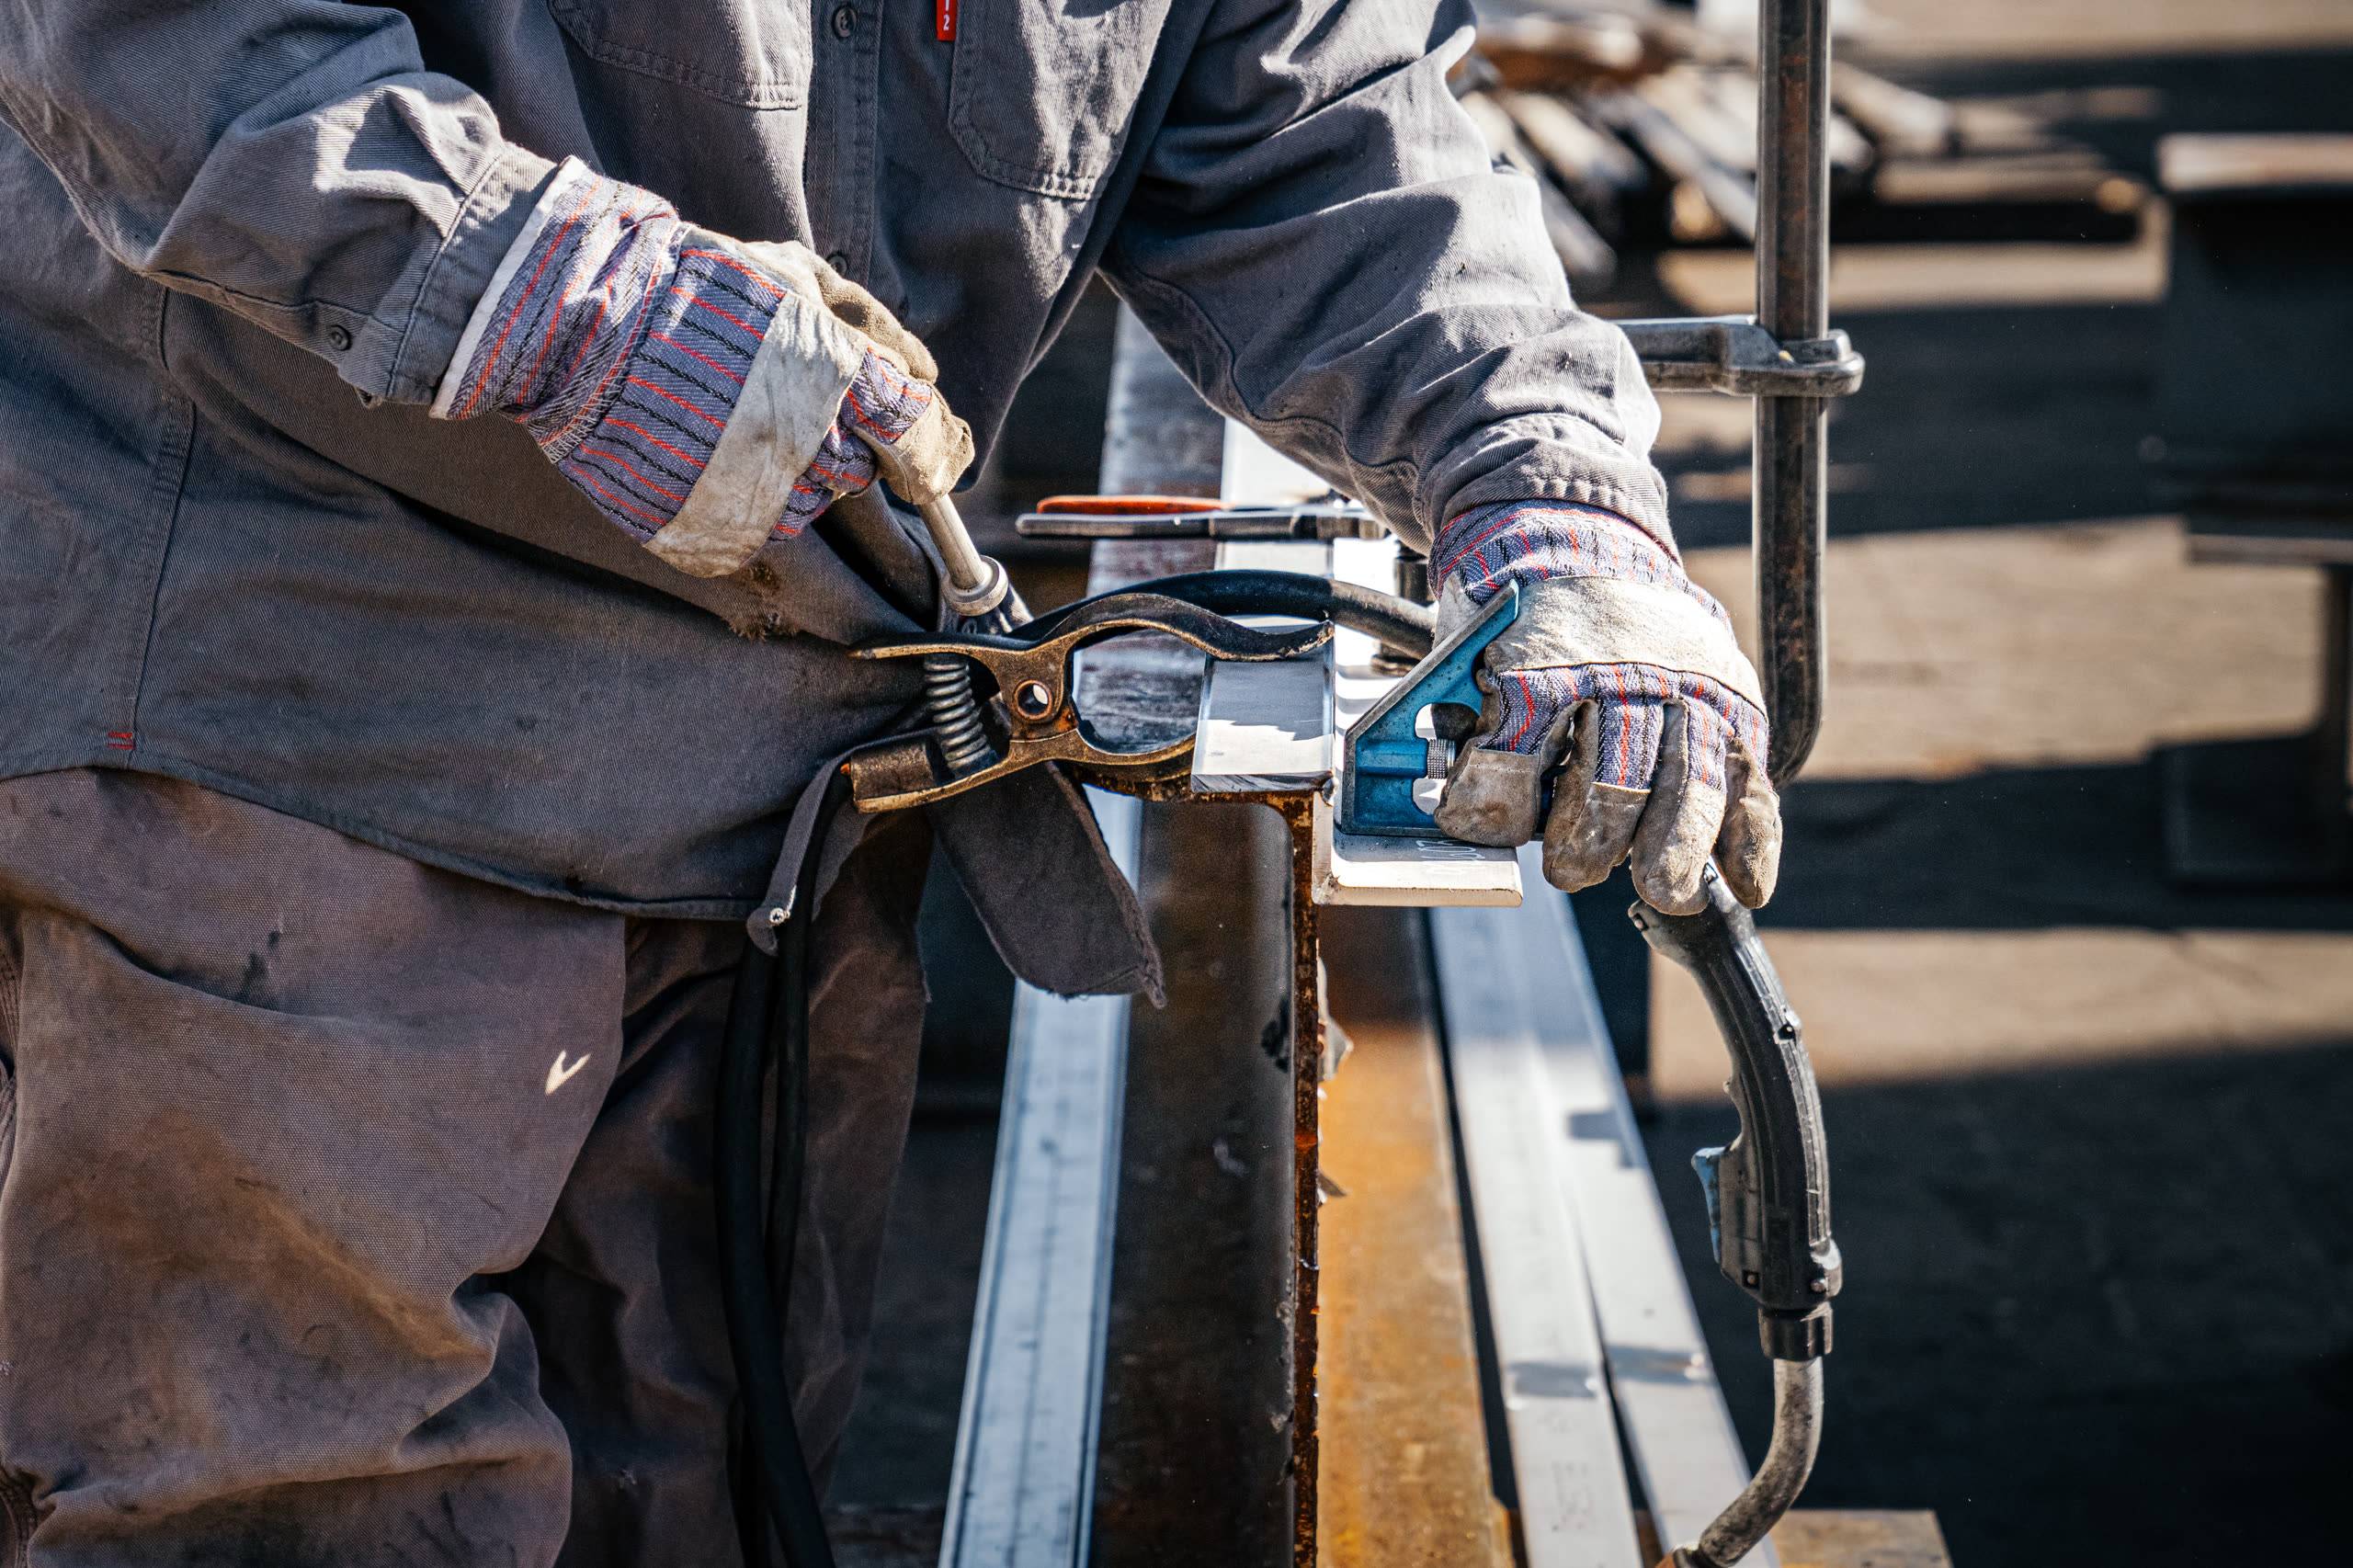
On a typical welded frame, the welding itself is a fraction of the labor. The rest is fitting: grinding a cope so a brace sits against a column, filing a bevel so a full penetration weld has somewhere to go, clamping, checking, adjusting, checking again.
None of that work is visible on the invoice as a separate line, which is exactly why it rarely gets designed out. It just appears as hours.
What the bevel head does
The laser cuts the bevel angle into the end of the section as it cuts the section to length, in the same operation, from the same program. A brace comes off the machine with its cope already matching the member it meets and its bevel already at the angle the weld procedure calls for.
The welder then does the thing a welder should be doing, which is welding, rather than spending the first half of the job making parts fit. Consistency follows too: the two hundredth joint is prepped identically to the first, which hand grinding never quite manages.
Design the assembly to fixture itself
The step beyond prep is letting the parts hold themselves together. Tab and slot features cut into both halves of a joint mean an assembly locates in one position and only one position, square, without a jig.
That is worth real money on anything built more than once, and it costs nothing extra to cut because the laser is already making that pass. Send us the model early and we will tell you where it applies.
Before you call
Questions we get asked
Not answered here? The fastest route is a phone call to the shop.
Got a drawing? Talk to the shop.
Call and we will talk it through, or send the scope and drawing set and we will get back to you with pricing and a schedule.